Buying Brass Turned Components That Fit Beyond the First Sample
Brass fittings can look deceptively simple on a purchasing spreadsheet. Two suppliers quote the same drawing, both samples screw into the mating assembly, and the lower unit price seems decisive. Differences often emerge later: a coating changes thread fit, a cross-hole retains chips, or a substitute alloy behaves differently in service. Buying a reliable turned component means defining what the assembled product needs and showing how those requirements will be checked.
This guide follows the purchase of a small threaded brass component from material selection to repeat orders. The examples are illustrative, rather than reports of particular customer projects. They apply to fittings, inserts, spacers and similar parts, although pressure-bearing or regulated applications require their own engineering and compliance review.
Start with the alloy and the environment
Brass is a family of copper-zinc alloys, not a single purchasing specification. Composition and supplied condition influence machining, strength, corrosion behavior and suitability for the intended application. A familiar material nickname is less useful than a complete grade designation linked to the relevant material specification. If the application restricts lead or involves drinking water, the purchasing team must establish the applicable requirements before comparing stock options.
Ask suppliers to identify the proposed alloy on the quotation and describe how material identity is retained through production. Free-machining grades can be attractive for turned components, but ease of cutting does not override the service requirements. Conversely, a proposed alternative should not be rejected simply because it machines differently. Evaluate the trade-off explicitly and approve any substitution through the drawing or purchasing specification.
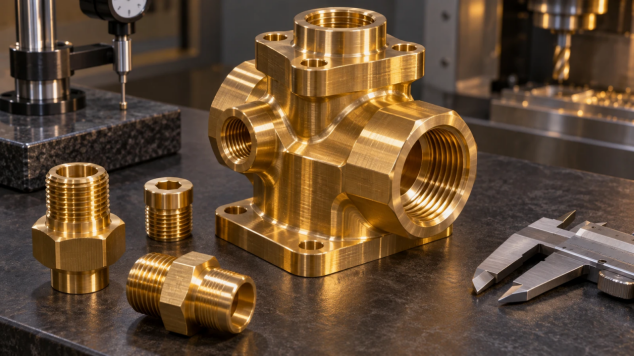
When evaluating a brass cnc machining manufacturer, start the discussion with the alloy, component function and critical interfaces. Jucheng’s brass material page describes CNC turning and milling for brass parts, including fittings and inserts. That provides a relevant starting point for a drawing review; the quotation should still identify the actual material and inspection scope for your component.
Threads are only one part of the fit
Assembly success depends on more than nominal thread diameter. Pitch, thread form, fit class, usable engagement and the relationship to adjacent locating surfaces all matter. State whether the thread is straight or tapered and which standard governs it. Include the mating component or a controlled interface drawing when the connection has a special sealing or alignment requirement.
Blind internal threads need room for tool entry, incomplete threads and chips. External threads require deliberate lead-ins, especially where operators assemble parts by hand. An oversized chamfer can remove useful engagement, while an uncontrolled burr can create misleading resistance during assembly. Drawings should distinguish a functional edge break from a general instruction to remove sharp edges.
Plating or other finishing adds another dependency. Decide whether thread acceptance applies before or after finishing, and specify masking where necessary. A sample tested before coating cannot establish that the delivered, coated part will fit. Agree on the finished condition early so the machinist and finishing supplier work to the same acceptance point.
Inspect the sealing feature as a feature
Leaks may be blamed on threads even when the sealing function belongs to a face, seat or elastomer groove. Identify the sealing mechanism and specify the surfaces that actually contact. Surface texture, scratches, concentricity and edge condition can all affect performance, but the necessary controls depend on the joint design. Avoid applying a demanding finish requirement to every surface without a functional reason.
For a sealing face, communicate the datum from which position or runout is controlled. For an internal seat, discuss inspection access before the first batch. If pressure testing is required, define the test medium, pressure, duration and acceptance criterion with the responsible engineer. A casual air check or visual examination should not silently replace the agreed functional test.
| Feature | Purchasing question | Useful acceptance evidence |
| Thread | Which standard and finished condition apply? | Specified gauge results and engagement check |
| Sealing face | Which marks or texture affect function? | Surface inspection and defined functional test |
| Cross-hole | Can chips remain inside the passage? | Cleaning method and accessible inspection |
| Locating diameter | Which datum controls assembly alignment? | Dimension and geometric inspection results |
| Coating | What thickness and masking are required? | Finishing record and checks after coating |
Turning strategy changes the quotation
Bar-fed turning can suit rotational components, but side holes, flats and off-axis details introduce additional operations. Combining operations may reduce handling, while a separate milling setup can be sensible for some quantities and geometries. Buyers need not dictate the machine arrangement; they should understand how the supplier preserves the relationship between critical features across operations.
Ask how a thin wall will be supported and whether a clamping surface is allowed to show marks. A very slender feature may require different stock allowance or a different sequence. These questions expose cost drivers more effectively than asking for a universal tolerance claim. They also create opportunities to simplify nonfunctional details before tooling, fixtures or production programs become expensive to change.
Quantity should be described honestly. A one-off prototype, a pilot batch and a recurring order justify different investments in tooling and inspection. Request prices at realistic quantity breaks and identify which setup costs are separate. Do not assume that multiplying the prototype price predicts the production price or that a low production quotation includes the same documentation as the sample order.
Cleanliness and packaging belong in the specification
Small passages and intersecting holes can retain chips or cleaning fluid. If the part will enter a fluid system, define the required cleanliness in terms your quality team can verify. The supplier needs to know whether a visual check is sufficient or whether a controlled extraction, particle assessment or other test is required. Leave the exact method open for discussion until the requirement is understood.
Packaging should protect the features that justified the machining effort. Loose contact between finished parts can mark a sealing face or damage a thread. Separators, caps or individual protection may be useful, but should be selected for the real handling risk. State whether protective materials must be removed before assembly and whether residue is acceptable.
Qualify repeatability before the next order
When comparing a brass precision turned components factory with another supplier, request a sample report tied to the drawing revision and material lot. Confirm how gauges are selected, which features receive recorded results and how nonconforming parts are handled. The aim is to make the accepted sample reproducible rather than to collect a long list of unrelated machine specifications.
Jucheng’s combination of brass turning and milling services is relevant when a component includes both rotational features and secondary machined details. The practical purchasing advantage is the opportunity to discuss those features in one manufacturing review. Verify the proposed operation sequence, finishing arrangements and documentation in the quotation instead of treating a general service description as a promise for every geometry.
Before releasing repeat production, resolve every sample deviation in writing. Retain the approved drawing, material specification, finish requirements and inspection plan together. A later change to alloy, stock form, coating or a critical machining operation should trigger an assessment of what needs rechecking. This discipline helps both parties distinguish a harmless production adjustment from a change that could affect assembly.
Send a supplier the drawing and model, expected order quantities, material designation, mating requirements and intended environment. Mark the few characteristics that determine acceptance. That package gives an engineering team enough information to propose a credible process and gives purchasing a fair basis for comparing quotations. It also makes the next conversation specific: which feature needs clarification, what evidence is missing, and what must be demonstrated before approval.